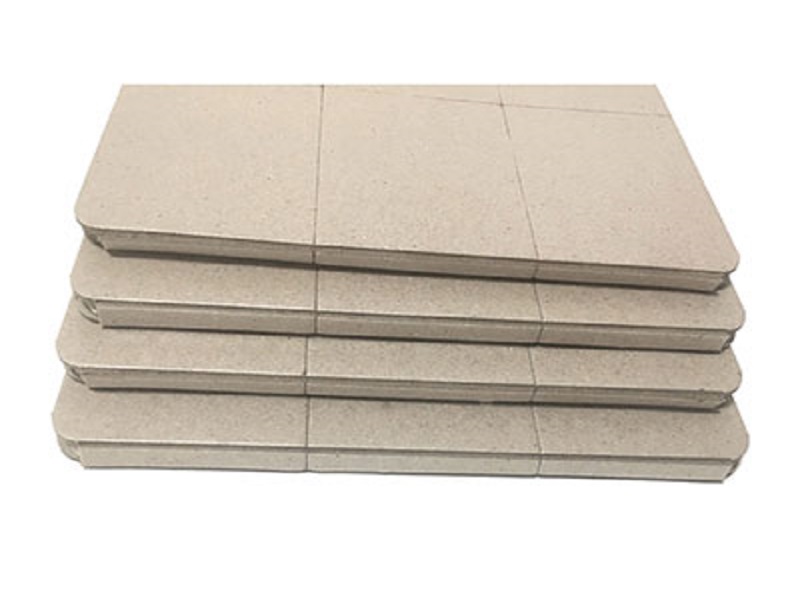
Duplex Board: Understanding Its Composition and Applications
When it comes to packaging materials, a duplex board is a widely used and versatile option. With its unique composition and characteristics, duplex board offers several advantages for various packaging and printing needs. In this blog post, we will delve into what a duplex board is, its composition, and its applications in the industry. By gaining a better understanding of duplex board, you can make informed decisions about its suitability for your packaging requirements.
Duplex Board Definition and Composition
Duplex board, also known as white lined chipboard, is a type of paperboard that consists of multiple layers. It typically comprises two layers: a top layer made from bleached chemical pulp and a bottom layer made from recycled fibers or waste paper. The layers are combined through lamination or adhesive bonding, resulting in a rigid and sturdy material. Duplex board is known for its smooth surface, strength, and excellent duplex board printing properties.
Variations in Coating
The duplex board comes in different variations based on its coating. The coating layer can be categorized into two types: coated duplex board (CCNB) and uncoated duplex board (UCNB). The duplex coated board has a thin layer of clay or other coatings applied to enhance its surface properties, making it ideal for high-quality printing and packaging applications. Uncoated duplex board, on the other hand, has no additional coating, which may be suitable for applications that require a more natural appearance.
Duplex Board Grammage and Thickness Table (230–450 gsm)
The stock range covers six bands between roughly 230 and 450 g/m², plus a lighter 193–200 g/m² band held for inserts and liners. Each band ships with a calliper window and a grammage tolerance; the figures below come from the grade data sheets published on the product pages.
Grammage (g/m²)
Thickness (µm)
CD grammage difference
Thickness difference
225–230
26–27.5
≤ 10 g
1 µm
243–250
29–30.5
≤ 10 g
1.2 µm
293–298
35.3–37
≤ 12 g
1.5 µm
342–348
41–43
≤ 15 g
2 µm
392–398
46.5–48.5
≤ 20 g
2 µm
442–448
53–55
≤ 20 g
2 µm
Two columns deserve attention when you write a purchase order. The CD grammage difference is how much the weight can vary across the machine direction of the sheet — on the heavier bands it opens up to 20 g, which matters if your die-cut blank is sized close to the board's stiffness limit. The thickness difference stays within 2 µm on every band, which is what keeps folding creases consistent across a full pallet.
Single-Coated vs Double-Coated Duplex Board
Trade usage splits duplex board into single-coated (C1S, coated white face over a grey back) and double-coated (C2S, both faces coated). The grades in the table above are single-coated: the print side carries a three-layer coating — top coat 10–12 g/m², medium coat 27–30 g/m² and primer 9–11 g/m², for a total coating weight of 50–55 g/m² — while the reverse stays uncoated grey.
Single-coated (C1S)
Double-coated (C2S)
Coated faces
Print side only; grey back
Both faces
Coating weight (print side)
50–55 g/m² in three layers
Grade dependent
Typical job
Folding cartons printed on the outer face
Premium print work where the reverse is also seen
Cost position
Standard export grades
Higher; quoted separately
For most folding-carton and sleeve work the single-coated construction is the right call, because the reverse face is glued or hidden inside the carton. If your design prints or shows the inside of the carton, ask for a double-coated grade before you lock the artwork — it is a separate stock item, not a coating you can add afterwards.
Whiteness and Brightness: What the Numbers Mean
Buyers often quote the two terms interchangeably; they measure different things. Whiteness describes the shade of the coated face — how close it sits to a neutral white — and the stock grades measure 78.5% or higher. Brightness is measured on the ISO scale at a defined wavelength and describes how much light the surface reflects; the stock grades measure 74% or higher on ISO brightness.
For practical purposes: a solid ink coverage job hides shade differences, but a light-tone or uncoated-wrap design shows them. If your brand colour sits close to white — pastel boxes, medical or cosmetic packaging — specify both figures on the purchase order and ask for a printed sample on the actual band you are buying, not a lab sheet.
Strength and Durability
One of the key advantages of a duplex board is its strength and durability. The combination of layers provides excellent stiffness and resistance to bending, making it ideal for packaging applications that require structural integrity. Duplex boards can withstand the rigors of storage, transportation, and handling, ensuring that your products remain protected throughout the supply chain. Its strength also makes it suitable for applications such as bookbinding, stationery, and display materials.
Printing and Packaging Applications
Duplex board is widely used in the printing and packaging industry due to its excellent printability and versatility. Its smooth surface allows for vibrant and detailed printing, making it suitable for packaging boxes, cartons, labels, and promotional materials. The duplex board's inherent rigidity ensures that the packaging maintains its structural integrity, offering a polished and professional presentation for your products. This durability is particularly crucial in duplex board food packaging, where maintaining shape and protecting contents is essential. Additionally, duplex board properties allow for die-cutting, folding, and creasing, enabling the creation of custom packaging designs tailored to your needs.
Environmental Considerations
The duplex board offers environmental advantages due to its composition. The use of recycled fibers or waste paper in the bottom layer contributes to resource conservation and reduces the demand for virgin materials. Additionally, the duplex board is recyclable, allowing for the creation of a circular economy and reducing waste. By choosing a duplex board for your packaging needs, you can align with sustainability goals and communicate your commitment to eco-friendly practices.
Duplex board is a versatile and reliable material widely used in the packaging and printing industry. Its composition, comprising layers of bleached chemical pulp and recycled fibers, provides strength, durability, and excellent printability. Duplex board finds applications in packaging boxes, cartons, labels, and various promotional materials. Its smooth surface and rigidity ensure a visually appealing presentation for your products while maintaining structural integrity. Additionally, the duplex board offers environmental advantages, aligning with sustainability goals. Consider duplex boards for your packaging needs and enjoy the benefits of this versatile material in enhancing your product packaging and branding efforts.
Need a quote? Send us your specification — material, thickness or grammage, sheet size and quantity — and we will confirm the closest stock grade, the tolerance it ships at and the lead time. Use the contact form or email tina@xiaolongpackaging.com directly.
Duplex Board FAQ
What grammages does duplex board come in?
The stock range runs across seven bands from 193–200 g/m² up to 442–448 g/m². Most folding-carton work sits between 230 and 450 g/m²; the lightest band is used for inserts, liners and shirt-board work. Each band's calliper and tolerance is published on its grade data sheet.
What is the difference between whiteness and brightness?
Whiteness measures the shade of the coated face against neutral white (78.5% or higher on stock grades); brightness measures light reflectance on the ISO scale (74% or higher). They are different test methods and different numbers — specify both if your artwork carries light tones.
Is duplex board single-coated or double-coated?
The standard export grades are single-coated: a three-layer coating totalling 50–55 g/m² on the print face, grey back uncoated. Double-coated board is a separate grade — request it explicitly if the inside of the carton will be printed.
Can duplex board be printed on both sides?
The coated face takes offset and digital print at packaging quality. The uncoated grey reverse accepts functional marks — batch codes, barcodes, stamps — but not quality print. If you need print on both faces, that is a double-coated grade, not a duplex board trick.
We use cookies to offer you a better browsing experience, analyze site traffic and personalize content. By using this site, you agree to our use of cookies.
Privacy Policy
 EN